Industrial Chemical Process: Overview of Modern Manufacturing Technologies
Industrial chemical processes are methods used to transform raw materials into useful products through chemical reactions, physical changes, and controlled manufacturing operations. These processes support many industries, including pharmaceuticals, agriculture, energy, food production, plastics, construction materials, and electronics.
Chemical manufacturing involves more than mixing ingredients. It requires careful control of temperature, pressure, concentration, reaction time, and material flow. Depending on the product, manufacturers may use heating, cooling, filtration, distillation, crystallization, drying, or chemical reactions to achieve the required results.
For example, fertilizer production uses chemical reactions to create compounds that support plant growth. Pharmaceutical manufacturing relies on carefully controlled chemical processes to prepare active ingredients. Water treatment plants use chemical methods to remove unwanted substances and improve water quality.
Modern industrial chemical processing combines scientific knowledge, specialized equipment, process engineering, and digital monitoring. The main objective is to produce consistent materials while managing energy use, environmental effects, and workplace risks.
How Chemical Manufacturing Developed
Early chemical production relied heavily on manual work and relatively simple equipment. As scientific understanding improved, industries introduced larger reactors, more accurate measuring instruments, and continuous production systems.
During the twentieth century, automation and advanced process control helped chemical plants manage complicated operations more consistently. Computer systems later made it easier to monitor equipment, analyze production data, and detect operating problems.
Today, industrial chemical engineering increasingly combines traditional reaction science with digital technologies, advanced materials, and resource-efficient production methods. This development allows manufacturers to study processes in greater detail and improve their understanding of how equipment behaves under different operating conditions.
Main Types of Industrial Chemical Processes
Different products require different manufacturing methods. The selected process depends on raw materials, product specifications, production volume, and safety requirements.
Batch processing: Materials are processed in separate quantities. This method is useful when production requires frequent changes or precise control of individual batches.
Continuous processing: Raw materials enter the system continuously while products leave at a controlled rate. It is common in large-scale chemical production.
Semi-batch processing: Some ingredients are added gradually while a reaction or other operation takes place inside a vessel.
Separation processes: Distillation, filtration, membrane separation, and crystallization help isolate useful substances from mixtures.
Thermal processing: Heating and cooling change material properties or support specific chemical reactions.
Electrochemical processing: Electrical energy drives chemical changes, including certain metal treatment and energy-storage applications.
Each approach has different operating requirements. Engineers choose a suitable method by considering product quality, process stability, equipment design, environmental impact, and operational risk.
Why Modern Chemical Manufacturing Matters
Supporting Essential Industries
Industrial chemical processes form the foundation of many everyday products and industrial materials. Their importance continues to grow as manufacturers respond to changing production needs, stricter safety expectations, and environmental challenges.
Chemical processing supports several important sectors:
Pharmaceuticals: Produces active ingredients and intermediate compounds used in medicine manufacturing.
Agriculture: Creates fertilizers, crop protection compounds, and soil treatment materials.
Energy: Supports fuel refining, battery materials, hydrogen production, and energy storage.
Construction: Produces coatings, adhesives, polymers, cement additives, and insulation materials.
Electronics: Supplies high-purity chemicals used in semiconductor and electronic component production.
Water treatment: Helps remove contaminants and control water quality in industrial facilities.
These industries depend on consistent chemical composition and reliable manufacturing conditions. Even small changes in temperature, contamination levels, or reaction time can affect the properties of a finished material.
Improving Quality, Safety, and Productivity
Modern chemical process technology helps engineers maintain better control over manufacturing operations. Automated instruments can measure pressure, temperature, flow rate, and chemical concentration throughout production.
This information supports several improvements:
Detecting abnormal operating conditions earlier.
Maintaining consistent product specifications.
Reducing avoidable material waste.
Improving equipment maintenance planning.
Supporting accurate production records.
Identifying opportunities to reduce energy and water use.
However, automation alone does not guarantee safe or efficient production. Equipment must be correctly designed, calibrated, maintained, and operated by trained personnel.
Comparing Traditional and Modern Processing
Manufacturing area | Traditional approach | Modern approach |
|---|---|---|
Process monitoring | Periodic manual readings | Continuous sensor monitoring |
Quality control | Sampling at selected stages | In-process measurement and laboratory testing |
Maintenance | Fixed schedules or breakdown response | Condition-based and predictive methods |
Production planning | Historical records and manual estimates | Digital analysis and process models |
Environmental monitoring | Periodic inspections | Integrated monitoring with documented checks |
The benefits depend on the plant, the chemicals involved, and the quality of implementation. Older equipment may remain appropriate for some operations, while other facilities may benefit from carefully planned upgrades.
Recent Developments in Chemical Manufacturing Technology
Artificial Intelligence and Process Automation
Artificial intelligence (AI) and industrial automation are becoming important parts of modern chemical engineering. These technologies can analyze operating data, identify unusual patterns, and help engineers understand complex relationships between process conditions and product quality.
For example, an AI-supported monitoring system may identify a gradual change in reactor temperature or equipment vibration. Operators can investigate the warning before the condition develops into a more serious problem.
AI can also support production scheduling, equipment maintenance, laboratory analysis, and energy management. Nevertheless, chemical plants must validate automated recommendations and keep appropriate human oversight, especially where incorrect decisions could create safety risks.
Digital Twins and Real-Time Monitoring
A digital twin is a computer-based representation of a physical asset or manufacturing process. It uses engineering models and operating data to help teams study how equipment behaves under different conditions.
Chemical engineers may use digital twins to:
Evaluate possible changes in operating conditions.
Study heat transfer and material flow.
Examine equipment performance.
Compare alternative production scenarios.
Support operator training and maintenance planning.
Connected sensors and industrial data systems make these models more useful by supplying information from actual plant operations. Their accuracy still depends on reliable measurements, appropriate models, and regular validation.
Greater Attention to Sustainability
Chemical manufacturers are increasingly examining how to reduce greenhouse gas emissions, improve energy efficiency, and recover useful materials from industrial waste.
Important areas of development include:
Electrification of selected heating processes.
Low-carbon hydrogen production.
Chemical recycling and material recovery.
More efficient catalysts and reaction pathways.
Water reuse and wastewater treatment.
Renewable or recycled feedstocks where technically suitable.
These approaches do not eliminate every environmental impact. Their overall benefits depend on energy sources, raw materials, process design, and the treatment of by-products.
Developments in India During 2026
India's chemical manufacturing sector has received attention through policy initiatives and discussions about digital transformation. On February 4, 2026, the Union Budget announced a scheme supporting three dedicated chemical parks, with an allocation of ₹600 crore for the 2026–27 financial year. The proposed parks are intended to provide shared infrastructure and support industrial development.
On May 5, 2026, industry reporting highlighted the growing role of AI, real-time analytics, and sustainability in India's chemical sector. These developments reflect a broader shift toward more connected and resource-conscious manufacturing.
These announcements indicate policy direction and industry priorities; they should not be interpreted as evidence that every facility has already adopted these technologies.
Laws, Regulations, and Safety Policies
Chemical Manufacturing Rules in India
Chemical plants must follow applicable national, state, and local requirements. The exact rules depend on the chemicals produced, the quantities stored, the plant's location, and the risks associated with its operations.
Important Indian legal frameworks include:
Environment (Protection) Act, 1986: Provides a central framework for environmental protection and pollution control.
Factories Act, 1948, and applicable state factory rules: Historically established workplace safety and health requirements for covered factories. The current legal position must be checked against the Occupational Safety, Health and Working Conditions Code, 2020, and its applicable commencement and implementation provisions.
Manufacture, Storage and Import of Hazardous Chemical Rules, 1989: Address specified hazardous chemicals, including requirements related to risk assessment, accident prevention, and emergency preparedness.
Chemical Accidents (Emergency Planning, Preparedness and Response) Rules, 1996: Establish arrangements for preventing and responding to chemical accidents.
Hazardous and Other Wastes (Management and Transboundary Movement) Rules, 2016: Govern specified hazardous waste handling, storage, transport, treatment, and disposal.
Environmental permissions, emissions limits, wastewater requirements, and hazardous waste authorizations may also apply. Facilities should verify current requirements with the relevant authorities rather than relying on general summaries.
Workplace Safety and Environmental Compliance
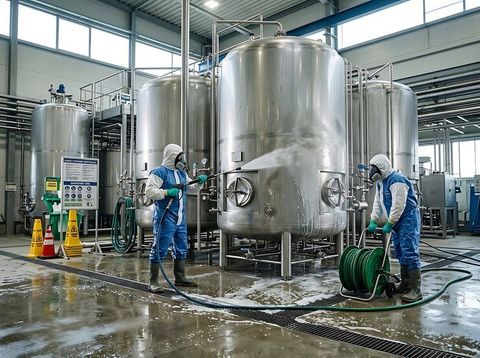
Chemical processing may involve flammable substances, corrosive materials, toxic gases, high pressure, and extreme temperatures. A suitable safety program should address these risks before production begins.
Common safety measures include:
Conducting process hazard assessments.
Providing suitable protective equipment.
Installing alarms and emergency shutdown systems.
Maintaining ventilation and gas detection equipment.
Training workers in chemical handling procedures.
Preparing emergency response and evacuation plans.
Keeping accurate chemical inventories and incident records.
Environmental compliance also requires suitable monitoring and waste management. Regulations can change, so facilities should maintain updated records and review their obligations periodically.
Tools and Resources for Chemical Process Engineering
Process Design and Simulation Tools
Chemical engineers use several types of digital tools to understand and improve manufacturing operations. These tools support planning, analysis, safety evaluation, and quality management.
Common categories include:
Process simulation software: Models chemical reactions, distillation columns, heat exchangers, and material flows.
Statistical analysis tools: Help identify quality variations and patterns in production data.
Computer-aided engineering tools: Support equipment design, process layouts, and engineering calculations.
Laboratory information systems: Organize test results, sample records, and quality documentation.
Industrial monitoring platforms: Display live readings from sensors and process control equipment.
Environmental assessment tools: Help estimate energy use, emissions, water consumption, and waste generation.
Engineers should select tools according to their technical requirements, data quality, and regulatory responsibilities.
Essential Engineering Calculations
Calculations help determine whether a chemical process can operate safely and consistently. Several are especially important in process engineering.
Calculation | Main purpose |
|---|---|
Mass balance | Tracks materials entering, leaving, and accumulating in a system |
Energy balance | Measures heat and energy entering or leaving a process |
Reaction yield | Estimates the amount of desired product obtained |
Heat transfer | Evaluates heating and cooling requirements |
Material flow rate | Determines how quickly substances move through equipment |
Emissions estimation | Helps assess releases associated with an operation |
These calculations provide a foundation for equipment selection and process improvement. Complex or hazardous systems also require detailed engineering reviews and appropriate validation.
Learning Resources and Professional Development
Beginners can develop their knowledge through chemical engineering textbooks, laboratory demonstrations, process safety manuals, technical training materials, and engineering case studies.
Useful learning subjects include:
Chemical reaction engineering.
Industrial separation methods.
Process instrumentation and control.
Industrial hygiene and chemical safety.
Environmental engineering.
Quality assurance and statistical process control.
Energy efficiency and sustainable manufacturing.
Practical learning should combine theoretical knowledge with supervised experience. Chemical reactions and industrial equipment should not be tested outside suitable facilities and established safety procedures.
Frequently Asked Questions
What Is an Industrial Chemical Process?
An industrial chemical process transforms raw materials into useful products through chemical reactions or physical operations. Examples include fertilizer production, petroleum refining, pharmaceutical ingredient preparation, and water treatment.
What Technologies Are Used in Modern Chemical Manufacturing?
Common technologies include automated process control, industrial sensors, process simulation, digital twins, advanced separation equipment, and AI-supported data analysis. The appropriate combination depends on the manufacturing process and its safety requirements.
How Does Automation Improve Chemical Processing?
Automation helps monitor operating conditions, maintain process stability, record production data, and identify unusual changes. It can support consistent quality and faster responses to equipment problems, but trained operators and reliable safety systems remain essential.
Which Regulations Apply to Chemical Plants in India?
Requirements may include environmental protection legislation, hazardous chemical management rules, factory safety provisions, and hazardous waste regulations. The specific obligations depend on the facility, substances handled, and applicable legal requirements.
How Can Chemical Manufacturing Become More Sustainable?
Manufacturers can examine energy efficiency, water reuse, waste reduction, improved catalysts, low-carbon energy, and material recovery. Each measure should be assessed for technical feasibility, safety, and its overall environmental impact.
Conclusion
Industrial chemical processes remain essential to modern manufacturing, supporting products and materials used in healthcare, agriculture, electronics, construction, energy, and many other sectors.